Economic analysis of compressed air generation — engineered stone manufacturer
At the customer's request, we carried out a comprehensive analysis of a compressor room with four compressors and a total power input of 240 kW. We also recorded pressure over time in the compressor room and at three locations by the production lines.
At the customer's request, we carried out a comprehensive analysis of a compressor room with four compressors and a total power input of 240 kW. We also recorded pressure over time in the compressor room and at three locations by the production lines.
The customer was experiencing air shortages and equipment shutdowns.
According to the manufacturer's specifications, these compressors should have achieved fairly favourable specific energy consumption in kWh/m3 of compressed air, around 0.1.
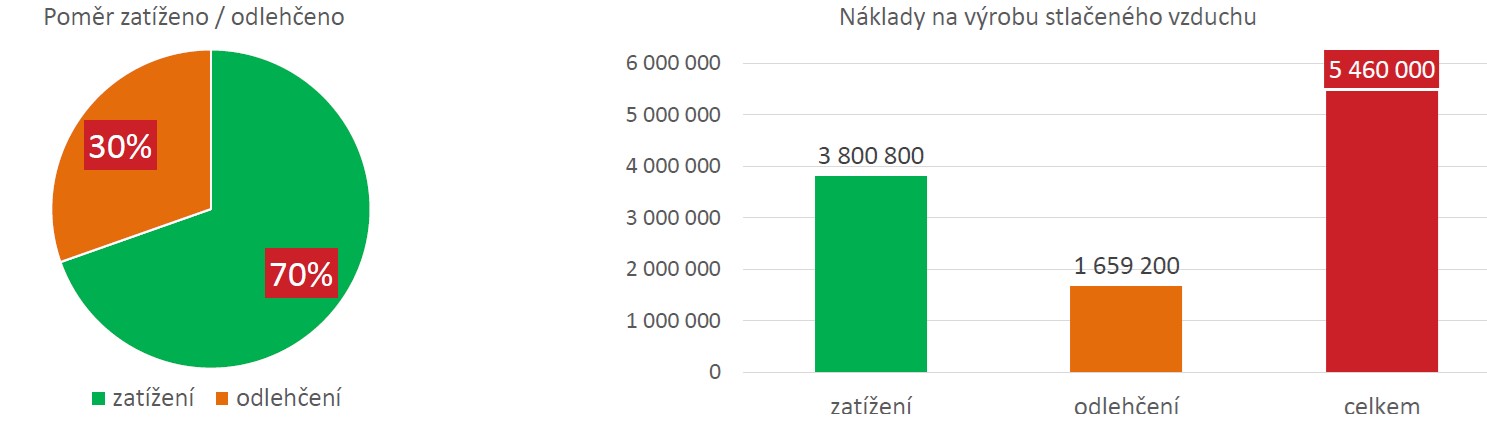
When installing the measurement equipment, frequent loading and unloading cycles already indicated a problem. After a week of measurements and data processing, we confirmed frequent cycling and a 2:1 ratio of electricity consumed under load to electricity consumed unloaded. One third of the electricity therefore produced no compressed air. The actual specific energy consumption was 1.33 kWh/m3, increasing electricity costs by approximately CZK 1 million per year.
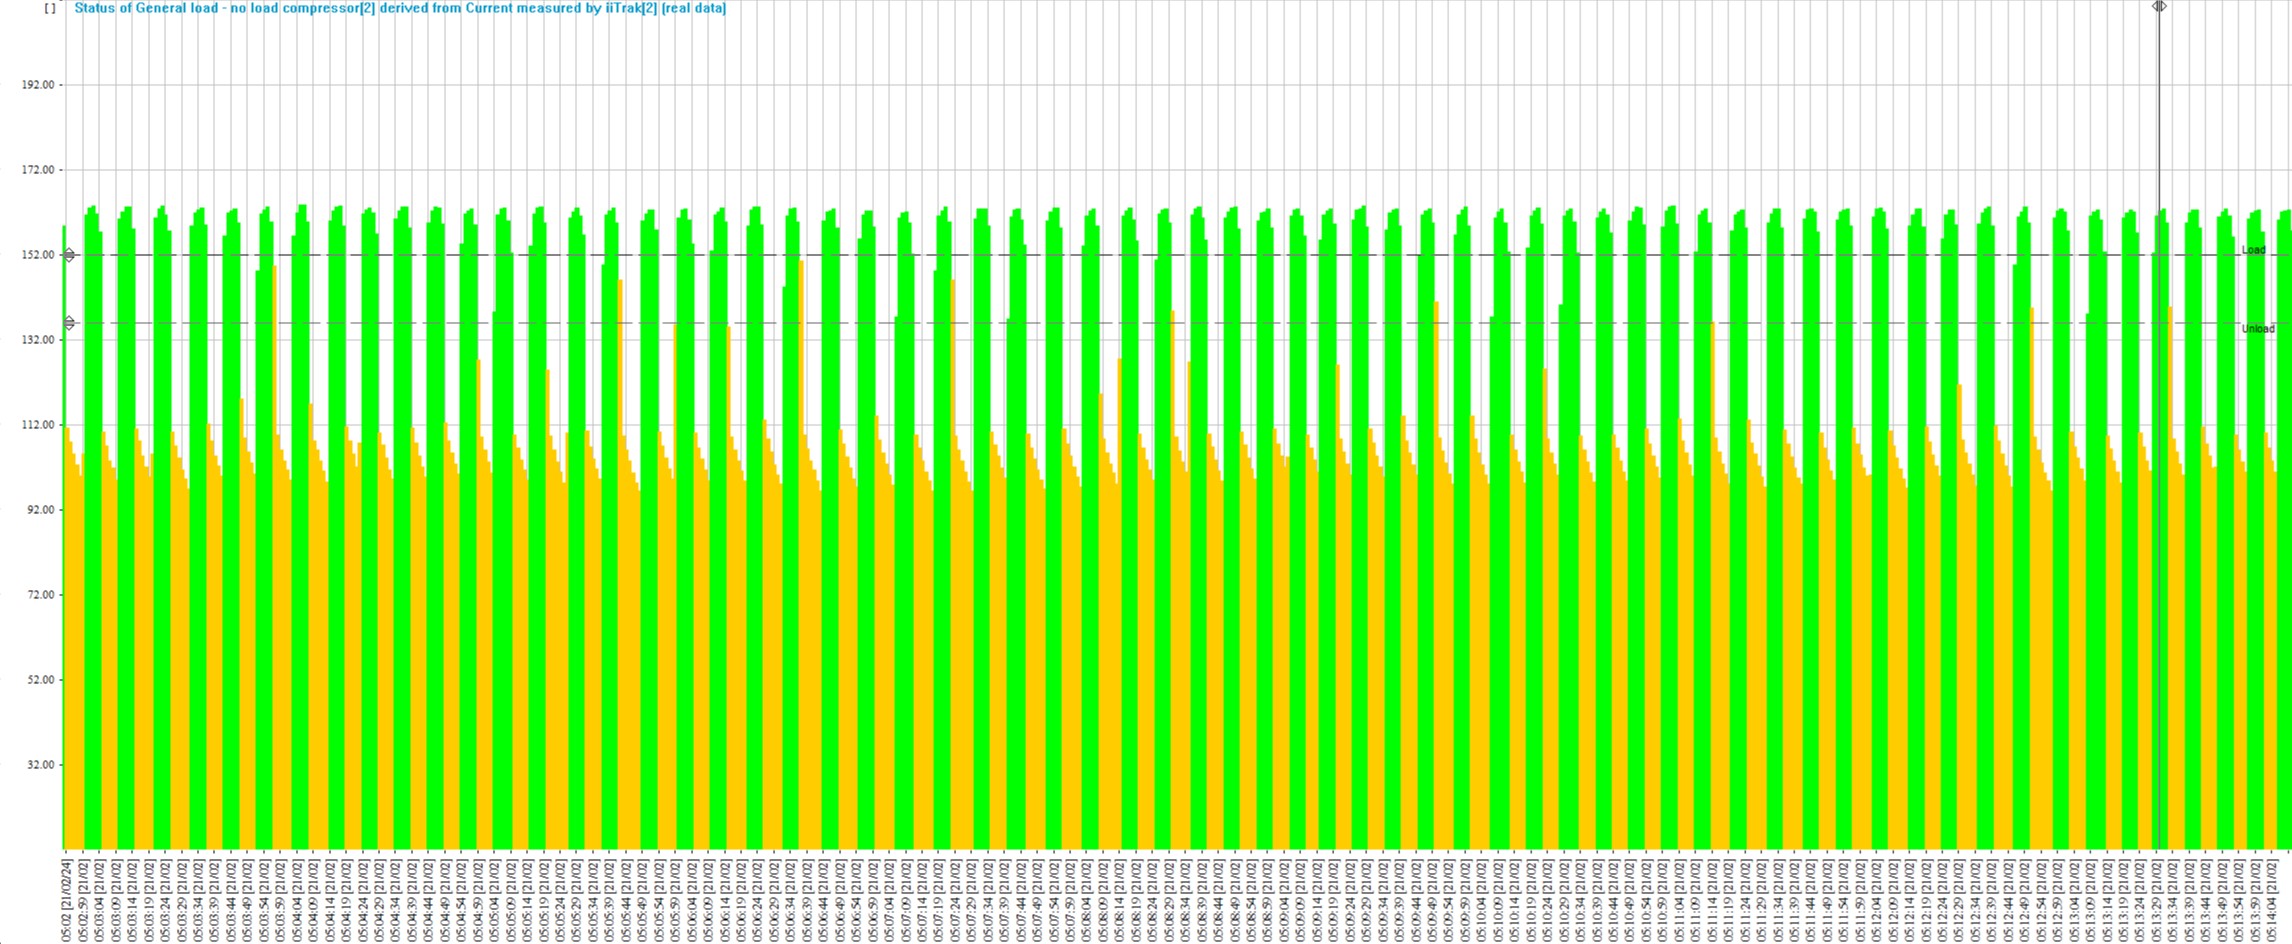
Example of compressor load/unload operation
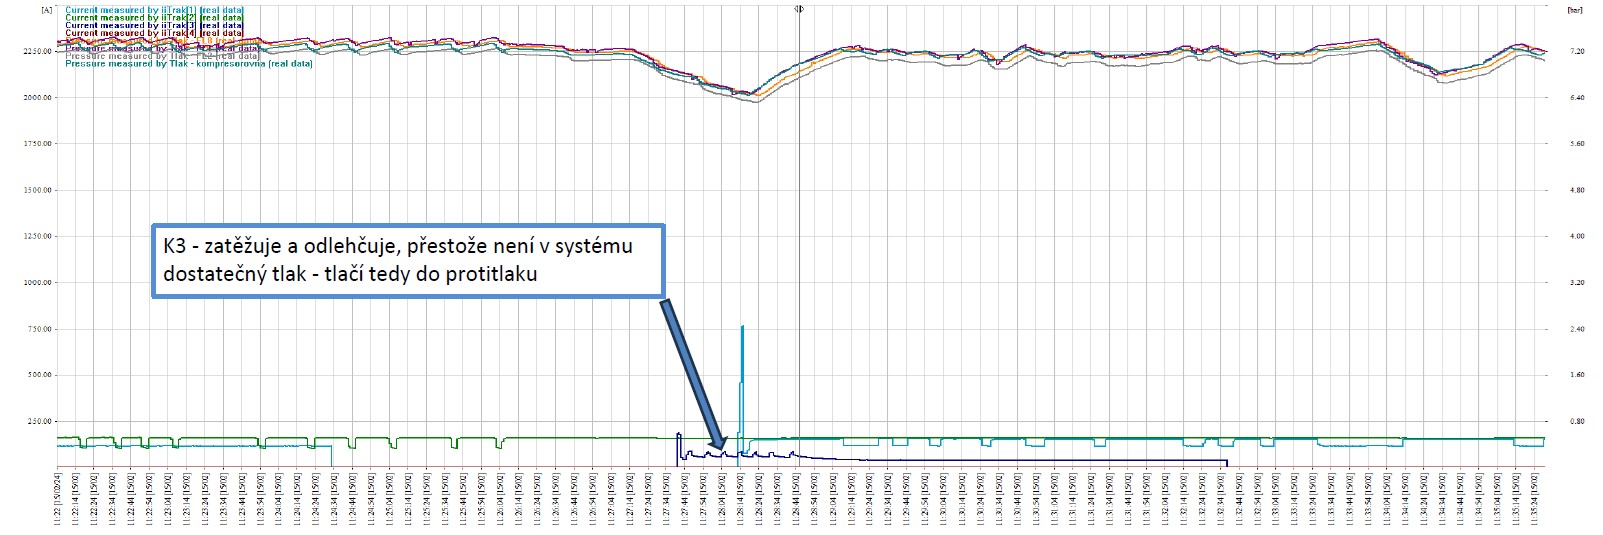
System pressure profile and compressor operation
Based on an analysing system pressure and compressor loading and unloading showed that some compressors unloaded even when system pressure was insufficient. Unwanted back pressure in the pipework was identified as the cause. Further measurements showed that the compressed air dew point (the temperature at which water condenses) was around or below 0 °C. Based on the analysis, we recommended having the dryers checked and repaired if necessary by a service company. It was subsequently confirmed that one dryer was cooling below freezing, causing its tubes to freeze and severely restrict airflow, thereby creating back pressure. This independent analysis confirmed the problem, identified its cause and enabled it to be eliminated, significantly improving compressor room operating costs and reducing equipment shutdowns caused by pressure drops.
Article photos
Show photosCollapse gallery